1. Executive Summary & Market Context
In the bulk water packaging sector, the 5-gallon container remains a critical component of global distribution. However, manufacturing non-spill, 55mm smart caps for 5-gallon bottles poses distinct engineering challenges. Traditional multi-cavity or legacy tooling often suffers from uneven cooling, inner plug thermal distortion, and flash generation along complex features such as internal pull-rings, tamper-evident bands, and side handles.
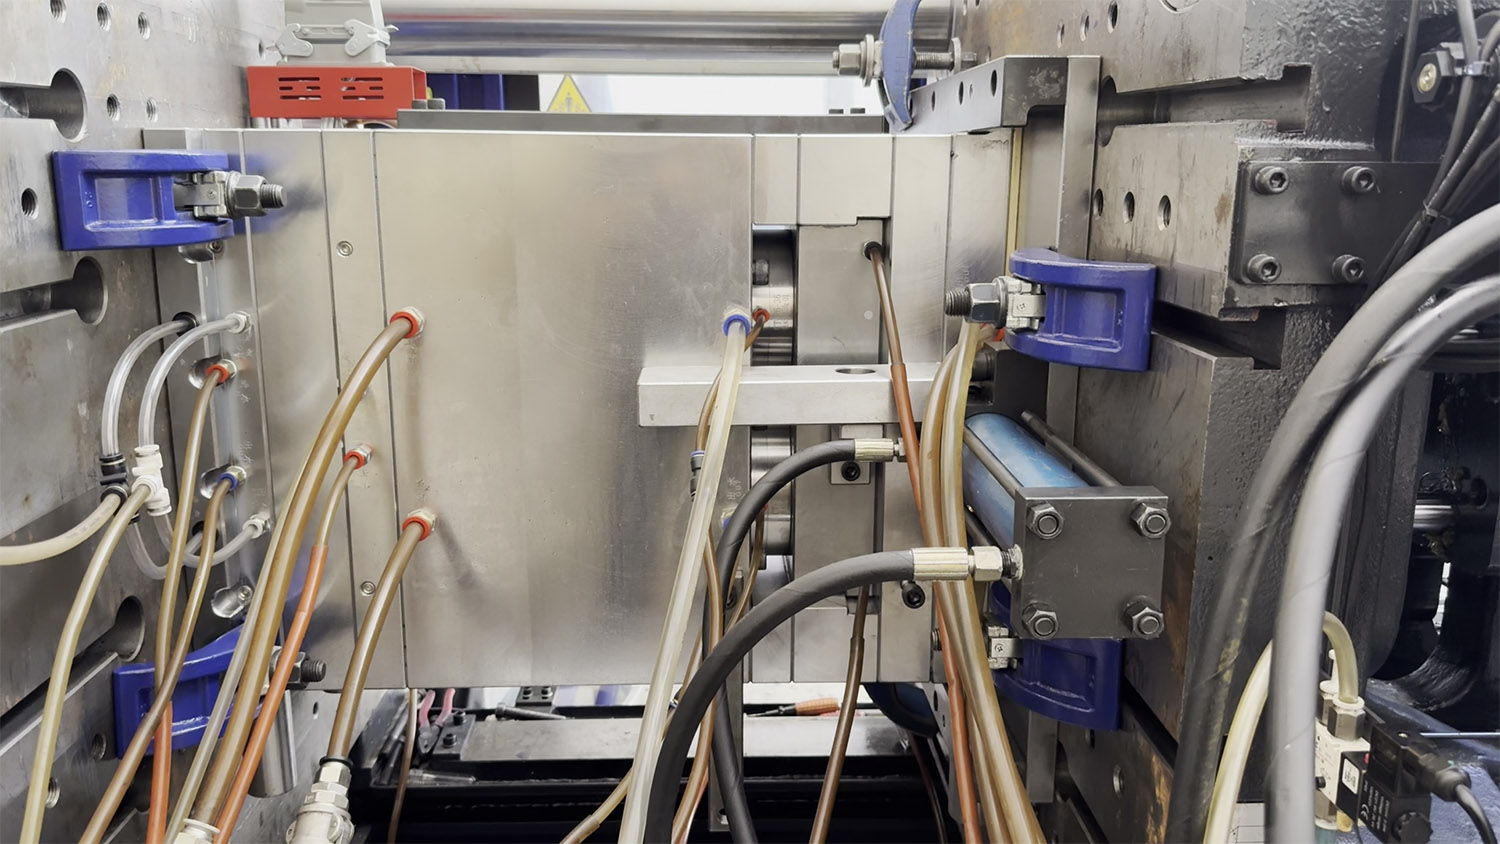
This engineering case study documents how Berni Mould assisted a major regional beverage bottler in converting a legacy 5-gallon cap production setup into a high-efficiency single-cavity optimized tooling process. By re-engineering the cooling circuit geometry, core ejection mechanism, and hot runner thermal balance, the client achieved a dramatic reduction in cycle time, eliminated leakage defects, and reduced operational energy consumption.
2. Problem Diagnosis: Bottlenecks in 5-Gallon Closure Tooling
The client was operating an outdated multi-cavity mold that frequently produced inconsistent cap dimensions, specifically around the inner sealing plug and the outer thread engagement area. The major defects encountered included:
- Seal Ovality & Distortion: Inadequate cooling at the center core caused thermal shrinkage, leading to micro-leaks during transport.
- Excessive Cycle Times: The heavy wall thickness of the 5-gallon cap neck required prolonged cooling times of up to 22 seconds.
- High Maintenance Overhead: Unbalanced runner pressure created uneven wear on neck rings and mechanical sliders.
3. Berni Mould’s Technical Solution
To resolve these challenges without increasing equipment footprint, Berni Mould’s engineering team engineered a custom high-efficiency single-cavity tool optimized for maximum thermal control and mechanical stability.
Core Steel Selection
Utilized Swedish ASSAB S136 stainless steel hardened to HRC 52–54, providing superior corrosion resistance and longevity under continuous high-pressure molding.
Conformal Cooling Design
Implemented 3D spiral cooling channels inside the core pin, ensuring direct heat evacuation from the thickest sections of the 5-gallon cap plug.
Hot Runner Optimization
Integrated a custom valve-gated hot runner system (compatible with YUDO/Mold-Masters standards) ensuring zero vestige and zero material drooling.
Key Technical Innovations:
- Precision Air-Assist & Stripper Plate Ejection: Ejection mechanisms were engineered to release the flexible PE material cleanly without deforming the internal valve membrane or outer tamper-evident seal.
- Taper Lock Core Positioning: Double taper locks were incorporated on the neck ring assemblies to ensure center-line alignment accurate within ±0.005mm, preventing wall thickness variation.
4. Performance Metrics & Production Results
Following the implementation of Berni Mould’s single-cavity high-efficiency tooling on an electric injection press, the client experienced immediate improvements across key operational metrics:
| Performance Metric | Legacy Multi-Cavity Tool | Berni High-Efficiency Single Tool | Delta / Improvement |
|---|---|---|---|
| Injection Cycle Time | 21.5 seconds | 11.8 seconds | 45% Reduction |
| Wall Thickness Tolerance | ±0.12 mm | ±0.005 mm | 95.8% Precision Gain |
| Defect / Leakage Rate | 2.8% | < 0.05% | Near-Zero Defect Standard |
| Tool Maintenance Interval | Every 250k shots | 1.5 Million shots | 6x Maintenance Extension |
5. Why Partner with Berni Mould for Cap & Preform Packaging Solutions?
At Berni Mould, we bridge the gap between mold design and final product performance. Whether producing 28mm water caps, PCO 1881 beverage closures, 38mm oil caps, or multi-cavity PET preform molds (ranging from 12 to 72 cavities), our engineering philosophy centers on long-term repeatability and cost optimization.
- Full Turnkey Ecosystem: Complete DFM analysis, mold flow analysis, hot runner manufacturing, and mold testing.
- Global Standard Compatibility: Designed to integrate seamlessly with major injection systems like Husky, Demark, Netstal, and standard hydraulic/electric presses.
- End-to-End Precision: Comprehensive quality control covering core components, heat treatments, and optical dimensional checks.
6. Conclusion
Transitioning to Berni Mould’s high-efficiency single-cavity tooling enabled the client to stabilize their 5-gallon water cap line while dramatically increasing overall line productivity. This case study highlights the importance of customized thermal management and precision tool geometry in closure manufacturing.

